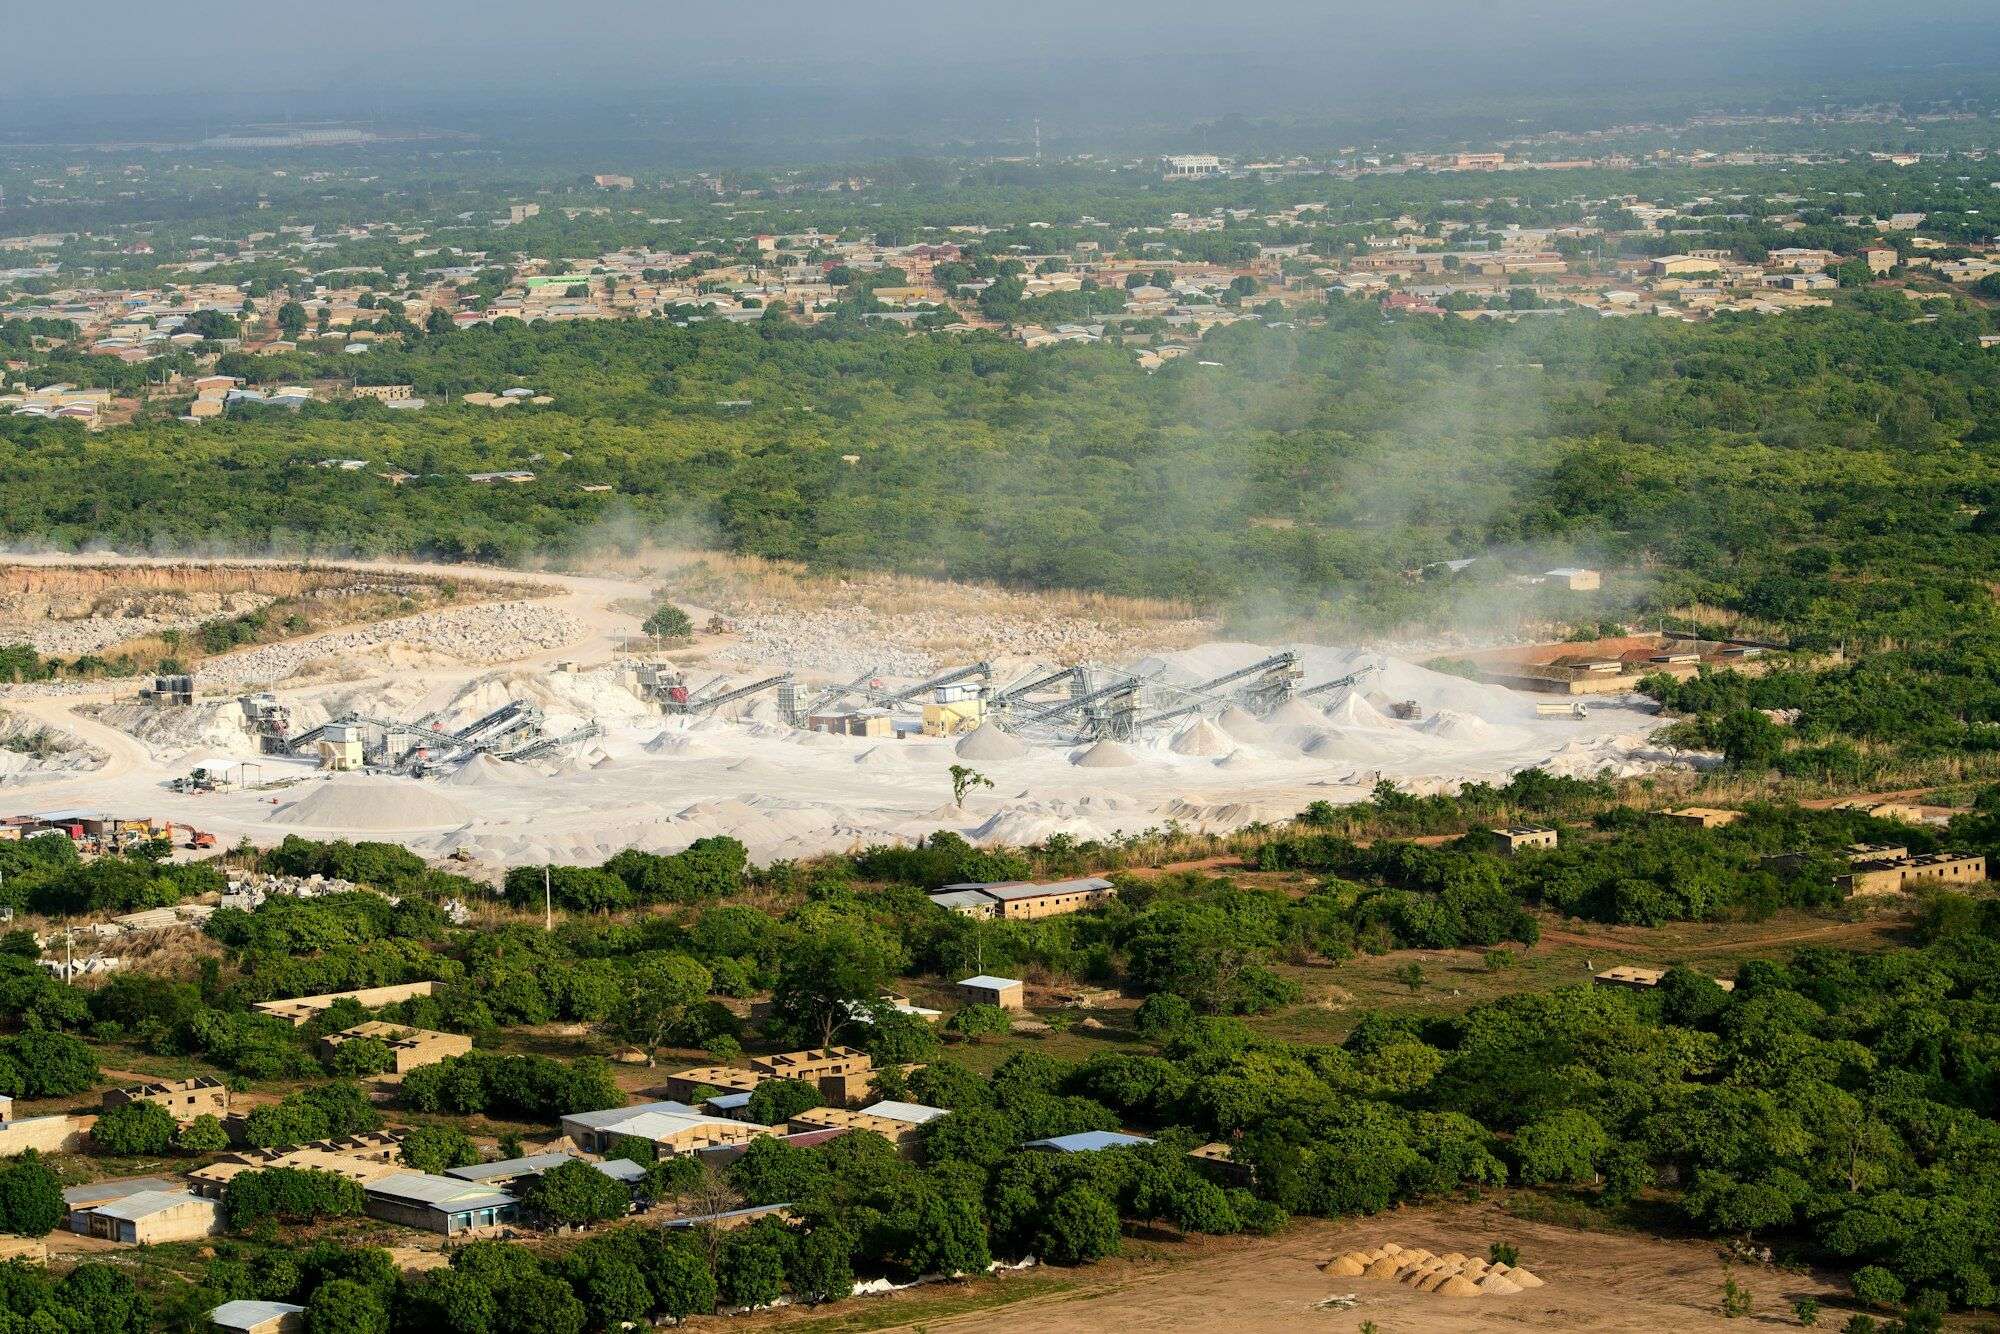
Quarry dust suppression control links each spray zone to the equipment it serves, so water is applied when material is moving and stops when it is not. On many plants, sprays are either left running continuously or switched manually, and neither approach matches the plant’s actual operation.
The cost of manually controlled sprays
The problems on a manually controlled system are familiar to most quarry and recycling operations:
- Water wasted on idle plant. Sprays left running during stoppages, breaks and loader delays consume water without suppressing any dust.
- Over-wetted product. Excess water at transfer points increases product moisture, which can cause screen blinding and product that falls outside its moisture specification.
- Dust when sprays are off. Sprays turned off during a stoppage are often not turned back on when the plant restarts.
- Inconsistent records. There is no record of when suppression was operating if a dust complaint or inspection arises.
Water is a significant cost for many sites, particularly those relying on trucked water, bores or limited storage through dry periods.
Why manual spray control does not work
A crushing and screening plant has many transfer points, and the dust generated at each depends on whether material is flowing, how much is flowing and how dry it is. An operator managing a plant from a control cabin cannot reasonably adjust a dozen spray valves as conditions change. The practical result is that sprays are set once and left, which is too much water at some times and too little at others.
Automatic quarry dust suppression control
The control system divides the plant into spray zones and switches each zone based on the running state of the equipment it serves. Where flow matters, spray intensity is scaled to throughput.
How it works
- 1
Detect running
The controller reads the running status of each conveyor, crusher and screen, and belt load where a belt scale is fitted.
- 2
Switch zones
Each spray zone opens when its equipment is running with material and closes after an adjustable delay when it stops.
- 3
Scale with conditions
Pulsed spraying or a variable speed pump adjusts water delivery to throughput and, where fitted, wind and dry weather.
- 4
Log operation
The system records when each zone operated, giving the site a record of dust suppression activity.
One contract, every trade licensed
Dust suppression involves pipework and water supply as well as controls. We carry out the electrical, instrumentation and controls work under QLD Electrical Contractor Licence 1513082. Pipework, valves on the water supply and any pump installation are carried out by a QBCC-licensed plumbing contractor that we engage and manage. You deal with one contract and one accountable lead, with every trade licensed for its part of the work.
What automatic control is worth
The benefit comes from three places: water no longer used on stationary plant, product moisture held closer to target, and consistent suppression that reduces dust events. Water savings are the easiest to estimate, because they follow directly from how often the plant stops.
Alternatives to automatic control
- Timers. Simple and inexpensive, but they spray on a schedule regardless of whether the plant is running.
- Wiring sprays directly to motor starters. Better than manual control, but every zone is on or off together and there is no adjustment or record.
- Chemical suppressants. Useful on haul roads and stockpiles, and can complement water sprays at the plant, but they still need controlled application.
- Separate trades. Engaging an electrician, plumber and controls contractor separately is possible, but coordination and accountability fall to the site.
For quarries also looking at pumping costs, dewatering pump VSD control applies similar principles to pit water.