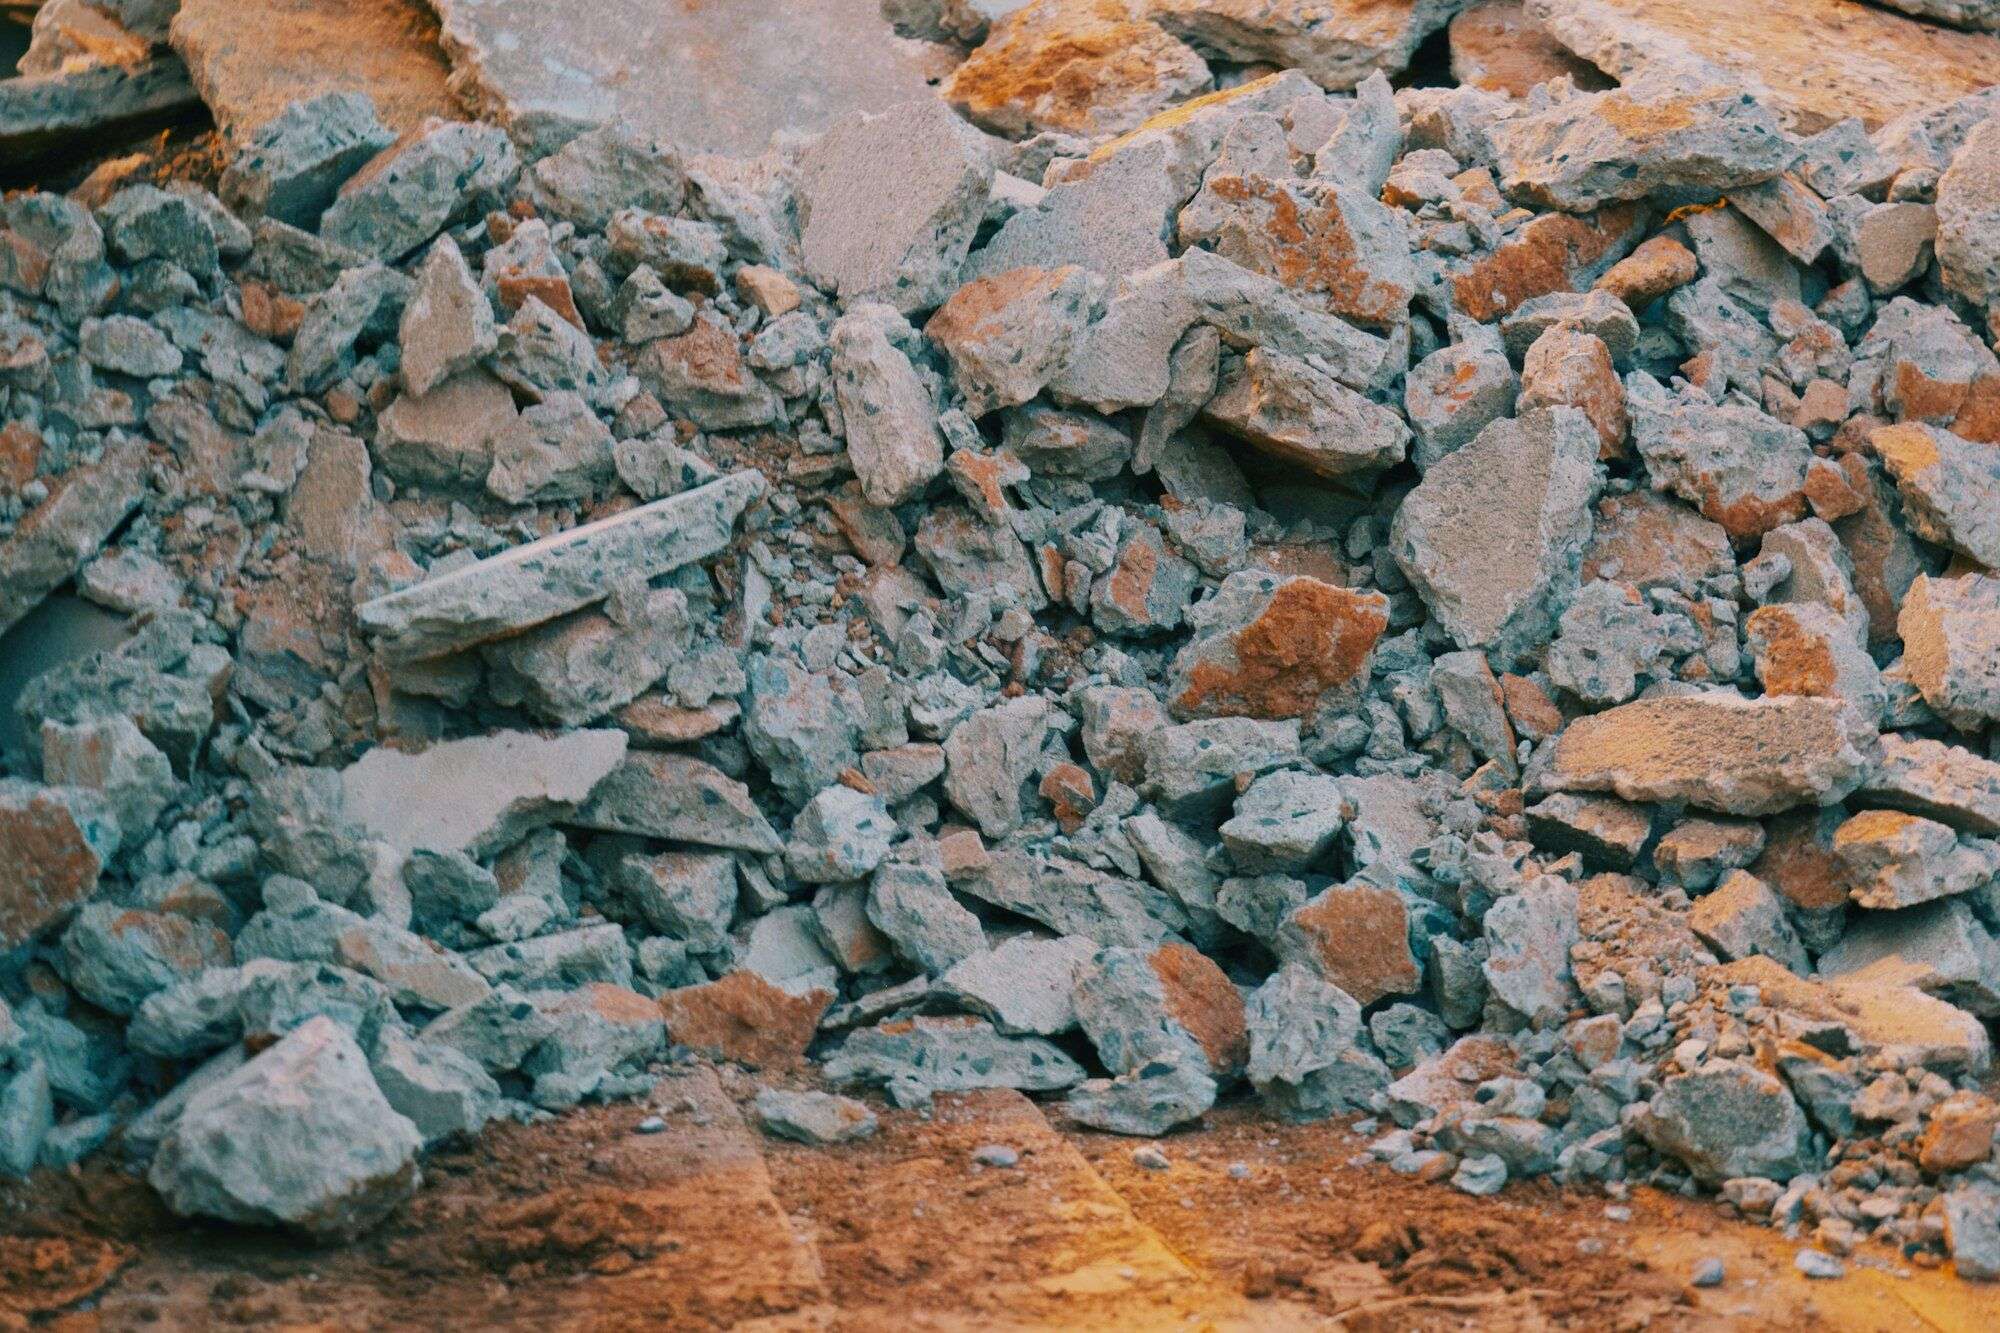
Concrete recycling crusher automation addresses a problem quarries rarely face to the same degree: feed that changes completely from one loader bucket to the next. A construction and demolition (C&D) recycler might move from clean concrete to brick and tile, then to asphalt millings or a load heavy with fines, all within an hour. A crusher fed at a fixed rate cannot respond to those changes, and the result is a plant that alternates between running light and stopping on overload.
Symptoms at a C&D recycling plant
The pattern on a recycling plant without automatic feed control is consistent:
- Overload trips and stalls. A run of dense concrete slabs loads the crusher beyond its capacity. The motor trips or the crusher stalls, and the plant stops while the chamber is cleared.
- Blockages at the feed opening. Bridging and blocked feed openings stop production and often require someone to work in a hazardous position to clear them.
- Running light. After a blockage or trip, operators reduce the feed rate as a precaution and the crusher spends long periods well below its capacity.
- Variable recycled product. Recycled aggregate and road base sold to a specification need consistent gradation, which is difficult to hold when the crusher load swings constantly.
Each of these increases the cost per tonne of recycled product and the wear on the crusher, feeder and conveyors.
Why mixed feed is difficult to control by hand
Concrete, brick, asphalt and soil break differently and load a crusher differently. A cubic metre of reinforced concrete slab presents a very different load to an impact crusher than the same volume of brick rubble. Moisture adds further variation, as wet fines pack and slow material flow through a jaw crusher.
A vibrating grizzly feeder set to one speed delivers roughly the same volume regardless of what is on it. The operator in the cabin sees the loader and the feeder, but has limited information about crusher load until an overload alarm or a stall. By then the only available action is to stop the feeder.
Concrete recycling crusher automation: how it works
Automatic feed control adjusts feeder speed continuously based on the crusher’s actual load. A variable speed drive (VSD) on the feeder allows it to run at whatever rate the crusher can accept, rather than at a fixed speed.
The control sequence
- 1
Measure load
Crusher motor current is measured continuously. On jaw crushers, a radar level sensor above the feed opening adds chamber level.
- 2
Set the feed rate
A programmable logic controller (PLC) compares load with a target and calculates the feeder speed needed to hold it.
- 3
Ease before overload
As load rises toward the crusher limit, feed is reduced progressively. It recovers automatically as the load falls.
- 4
Interlock the plant
The feeder is interlocked with the magnet, discharge conveyor and screens, so feed stops if downstream equipment is not running.
The system responds to the crusher, not to a fixed schedule, so it adapts to each load as it arrives. Operators retain manual control and can override the automatic mode at any time. For quarry cone crushers, where the aim is to keep the chamber full rather than to manage overload, see cone crusher choke feeding.
What steadier feed is worth
Published results for crusher feed control are encouraging. Aggregates Business reports that one quarry operator increased crusher throughput by 9% using adaptive feed control that slows rather than stops the feeder. On recycling plants, much of the benefit comes from reducing stoppages, which the throughput figure alone does not capture.
Demand for recycled aggregate is closely tied to construction activity. A report for the Queensland Department of Resources and Cement Concrete and Aggregates Australia forecasts Queensland quarry material demand to rise 24% to 66.2 million tonnes by 2029 to 2030, and recycled product competes in parts of that market.
Other ways to manage variable feed
- Pre-sorting and blending. Good stockpile management and loader practice reduce variation and remain worthwhile. They do not remove variation within a load.
- A larger crusher. Adds capacity at significant cost, but an oversized crusher on variable feed still runs light for much of the time.
- Manufacturer automation. Modern mobile crushers often include feed control in their own systems, and these are a sound choice where fitted. Older and fixed plants usually have none.
- A large systems integrator. Suited to new complete plants. For a single crusher circuit, the overheads are often out of proportion to the work.